Equipment / Handheld laser welding
Handheld Fibre Laser Welding Machine
A handheld welding series reference. Match power, joint geometry, shielding gas and test conditions to the actual workpiece.
- Source-listed power options
- 1000 / 1500 / 2000 / 3000 W
- Source-listed work method
- Continuous
Handheld welding with application-specific validation.
The supplied introduction describes handheld laser welding for precision welding work, including electronic components and the repair or manufacture of precision mechanical parts. Suitability for a particular component must be assessed through its material, joint and process requirements.
The parameter sheet names a handheld fibre laser welding series with four power options and continuous operation. It does not identify a separate commercial model code for each power variant.
Welding head, wire feed & function selection.
The properties document includes the text “Wobble welding head (optional wire filler)”, but this is incorrectly entered against the “Laser Wave length” label. The text is retained only as a configuration item to clarify; it is not a wavelength value.
The introduction describes welding, cutting, cleaning and weld-cleaning functions through nozzle changes. This is a source-described series capability, not confirmation that every accessory or mode is supplied in a particular configuration.
Confirm the delivered head, nozzles, wire feeder, enabled modes, software and supported consumables. Precision and surrounding-material protection statements in the introduction are not treated as measured guarantees.
Handheld series reference parameters.
Swipe horizontally to read every column.
| Parameter | Supplied entry | Review boundary |
|---|---|---|
| Product reference | Handheld fibre laser welding | No individual power-variant model codes provided. |
| Laser power | 1000 / 1500 / 2000 / 3000 W | Select the actual offered configuration. |
| Work method | Continuous | Source entry. |
| Working voltage | AC 220 V / AC 380 V; 50 / 60 Hz | Confirm phase, load, protection and destination requirements. |
| Shielding gas | N₂ / Ar | Material and process suitability require agreement. |
| Gap: swing welding | <0.5 mm | Source reference, with process conditions not specified. |
| Gap: swing with wire filler | <1 mm | Source reference, optional wire-feeder configuration must be confirmed. |
| Laser wavelength | Pending confirmation | Source row contains welding-head text instead of a wavelength value. |
Do not infer wavelength, maximum penetration, electrical compatibility or accessory inclusion from this source sheet. The final specification must identify the selected power and complete configuration.
Accessories, utilities & workstation information.
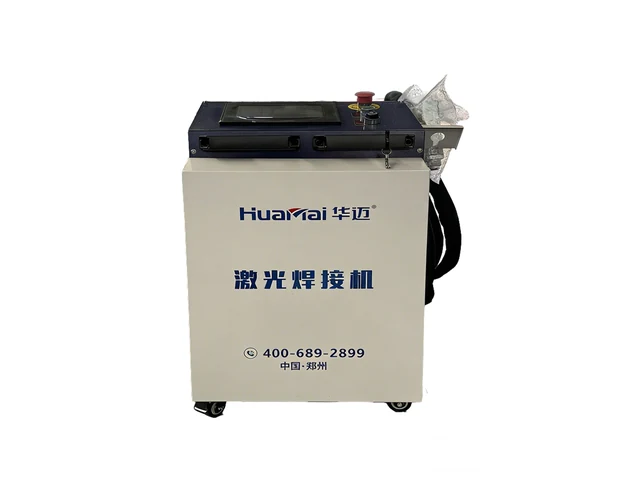
The series photograph shows supplied equipment imagery. The properties table mentions a wobble welding head and optional wire filling.
A dimensioned installation drawing, cable/torch reach, cooling-system specification, electrical load, gas consumption, consumables list, protective equipment requirements and model-specific safety documentation remain to be confirmed. No dimensions or safety classification have been invented.
Source thickness references need test conditions.
Swipe horizontally to read every column.
| Power | Stainless / carbon steel source entry | Galvanised / “aluminum steel” source entry |
|---|---|---|
| 1000 W | ≤2 mm | ≤1.55 mm |
| 1500 W | ≤3 mm | ≤2 mm |
| 2000 W | ≤5 mm | ≤3 mm |
| 3000 W | ≤8 mm | ≤4 mm |
These are unverified “recommended welding thickness” entries in the supplied document, not guaranteed weld penetration or joint acceptance limits. The phrase “aluminum steel” is ambiguous and needs correction. Material grade, joint type, fit-up, filler, gas, preparation, travel speed and inspection criteria are not provided.
Agree a representative joint trial and inspection criteria before selecting the power. No weld-strength, leak-rate, productivity or quality result is supplied for this record.
Assess the joint and component.
The introduction names electronic components and precision mechanical-parts repair or manufacture. The properties table gives thickness references for stainless and carbon steel and also contains ambiguous galvanised/aluminium wording.
A material name in a table is not a verified process approval for every component. Confirm alloy, coating, joint type, accessibility, required quality and relevant acceptance method for the actual application.
Configuration & process constraints.
The properties document states that customisation can follow customer requirements. Its gap references distinguish swing welding from swing welding with wire filling.
Confirm the intended welding process, wire feed, gas, torch/accessory set, electrical supply and supported materials. The laser-wavelength field and the ambiguous material term require supplier correction. Neither is filled using assumed values.
Separate company documents from weld validation.
Company management-system documents do not establish that a particular weld joint, power variant or delivered configuration has passed a specific test.
Review company and product-document scope →
No identified customer project, destructive/non-destructive inspection report or conformity match for a named power variant is established by this page.
Operation, training & maintenance support.
The service programme includes operation and software training, maintenance, troubleshooting, technical support and spare-parts supply. Installation guidance is also described.
Training arrangements, consumable supply, on-site responsibilities, warranty and delivery terms must be agreed for the selected configuration.
Describe the welding requirement.
Include material grade, thickness, joint type, fit-up, access, quality requirements and the power variant under consideration. Use sample information in this review.